65 Amp Plasma Cutter: What It Cuts and How to Choose One
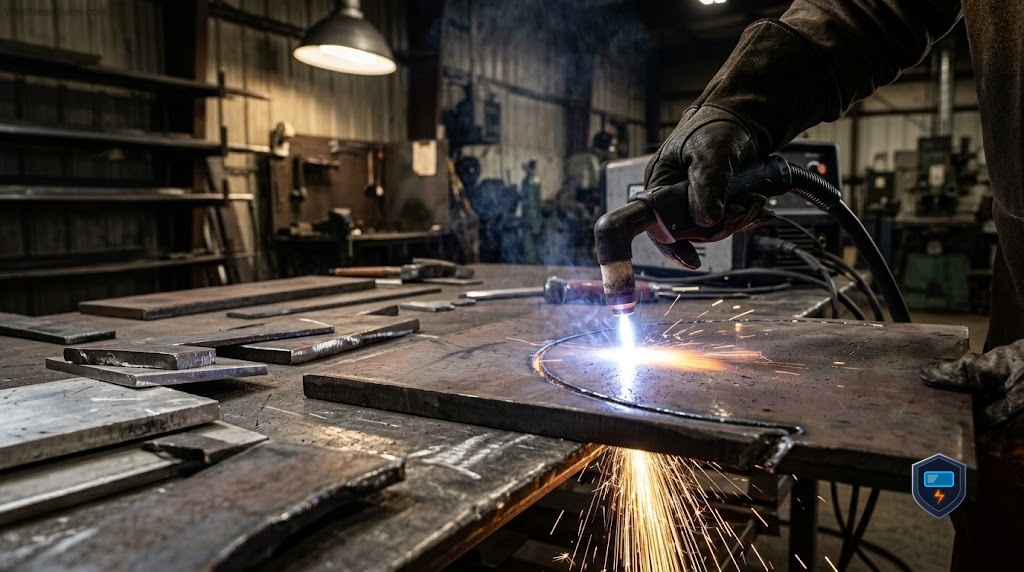
The 65 amp plasma cutter is the machine you graduate to when a 50-amp cutter stops keeping up, when you regularly cut thicker plate, need a higher duty cycle for steady work, or want a source you can put on a CNC table later. It is a serious-shop tool that still stays within reach of a well-equipped garage. But 65 amps buys real capability only if the machine and its support, air, duty cycle and torch, are right. Here is what a 65 amp plasma cutter cuts and how to choose one.
What a 65 amp plasma cutter cuts
A 65-amp machine has a recommended (clean) cut capacity of around 3/4 inch on mild steel, a maximum around 1 inch, and a severance capacity up to about 1-1/4 inches cut slowly. It also pierces up to roughly 5/8 inch to start a cut in the middle of a plate. That covers heavier plate fabrication, structural work, and thicker stainless and aluminum, a real step beyond the 1/2-inch range of a 50-amp machine. The class benchmark is Hypertherm’s Powermax65 SYNC.
Why serious shops step up to 65 amps
Three things push people from 50 to 65 amps:
- More thickness: 3/4 inch clean versus 1/2 inch, with margin for heavier work.
- Higher duty cycle: the ability to cut longer before cooling, which matters for steady production.
- Mechanized potential: many 65-amp systems accept a machine torch and CNC interface, so the same source can drive a cutting table later.
If any of those describe your work, the step up pays off.
The torch and consumables
A quality 65-amp machine uses a good pilot-arc torch. The Powermax65 SYNC, for example, uses a single-piece cartridge consumable that combines the electrode, swirl ring and nozzle, simplifying changes, reducing setup errors, and tracking its own usage. However the consumables are packaged, keep them matched to your amperage and fresh, since worn consumables widen the kerf and bevel the edge on any machine.
Duty cycle and air supply
At 65 amps you are cutting thicker and often longer, so both duty cycle and air matter more:
- Duty cycle: check the rating at 65 amps, and confirm it suits how long you cut in one go. Steady or mechanized work wants a high duty cycle.
- Air supply: a 65-amp machine needs a solid supply of clean, dry, oil-free air (the Powermax65 SYNC wants roughly 6.7 CFM at around 90 PSI, minimum 75 PSI). Size the compressor generously (about 1.5 times the rated CFM) and add a filter/dryer.
Undersized air is the most common reason a capable 65-amp machine cuts poorly.
How to choose a 65 amp plasma cutter
- Confirm the real cut rating (about 3/4 inch clean) matches your typical metal.
- Check the duty cycle at 65 amps against how long you cut.
- Prefer a pilot-arc torch with easy consumables (like a single-piece cartridge).
- Confirm mechanized capability if you may add a CNC table.
- Size the air supply with headroom and a filter/dryer.
- Buy a supported brand for consumables and service.
The verdict
A 65 amp plasma cutter is the serious-shop step up: around 3/4 inch of clean cutting, a higher duty cycle, and the option to go mechanized. It is worth it only when your work actually calls for that capability.
Three things to hold onto. Match the roughly 3/4-inch clean cut capacity to your typical metal, stepping up from 50 amps because you regularly cut thicker plate, not just for a bigger number. Weigh duty cycle and mechanized potential, since a high duty cycle suits steady production and a machine-torch-capable source can drive a CNC table later. And size the air supply generously with a pilot-arc torch and fresh consumables, because undersized or moist air is the top reason a capable 65-amp machine cuts poorly.
When your work has outgrown 50 amps, a 65-amp machine like the Powermax65 SYNC is the right next step; if you rarely exceed 1/2 inch, a 50-amp machine is the smarter buy.
Frequently asked questions
What can a 65 amp plasma cutter cut? A recommended clean cut of about 3/4 inch on mild steel, a maximum around 1 inch, and a severance capacity up to about 1-1/4 inches cut slowly. It pierces up to roughly 5/8 inch and handles heavier plate, stainless and aluminum.
Is a 65 amp plasma cutter worth it over a 50 amp? Only if you regularly cut thicker than 1/2 inch, need a higher duty cycle for steady work, or want the option to add a CNC table later. If you rarely exceed 1/2 inch, a 50-amp machine is the smarter, lower-cost buy.
What air supply does a 65 amp plasma cutter need? A solid supply of clean, dry, oil-free air, roughly 6.7 CFM at around 90 PSI (minimum 75 PSI) on the Powermax65 SYNC. Size the compressor generously (about 1.5 times the rated CFM) and add a filter/dryer, since undersized air is the top cause of poor cuts.
Can a 65 amp plasma cutter be used on a CNC table? Many can, if the machine accepts a machine torch and has a CNC interface. This mechanized potential is one reason shops step up to 65 amps. Confirm machine-torch and CNC capability before buying if a cutting table is in your plans.
What is a single-piece cartridge consumable? A consumable that combines the electrode, swirl ring and nozzle in one unit, used on machines like the Powermax65 SYNC. It simplifies changes, reduces setup errors, and can track its own usage, making consumable management easier than loose parts.
What duty cycle does a 65 amp plasma cutter have? It varies by model, so check the rating at 65 amps. Steady production and mechanized cutting want a high duty cycle so the machine cuts longer before cooling. Confirm the rating suits how long you typically cut in one go.
How thick can a 65 amp plasma cutter pierce? Up to around 5/8 inch on a machine like the Powermax65 SYNC, letting you start a cut in the middle of a plate rather than from an edge. Piercing capacity is always less than the maximum cut capacity.
Which 65 amp plasma cutter is best? Hypertherm’s Powermax65 SYNC is the class benchmark, with a 3/4-inch cut capacity, single-piece cartridge consumables, mechanized capability and strong support. Whatever you choose, prioritize a pilot-arc torch, adequate duty cycle and air, and a supported brand for consumables.